Nut Snack Wholesale Factory: A Complete Guide to Sourcing Premium Products from U100, Factory-Direct Excellence
Sep 17, 2026
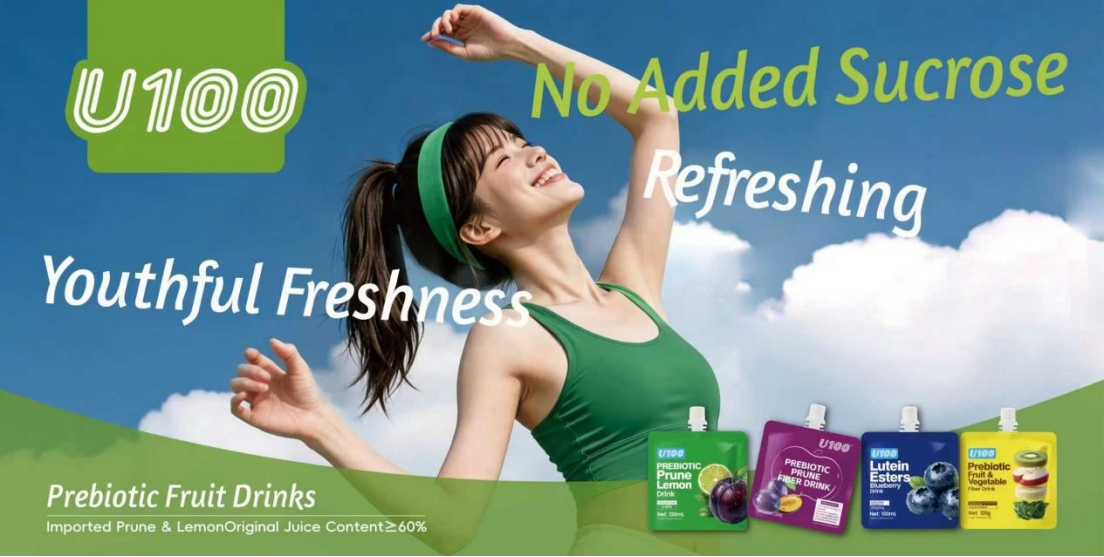
Linyi, Shandong Sep 16, 2026 (Issuewire.com) - Navigating the global snack food market requires a strategic approach to procurement, especially when sourcing high-volume offerings like nuts and dried fruits for retail chains. For international B2B buyers, selecting the right Nut Snack Wholesale Factory involves evaluating more than just price points; it demands a rigorous examination of supply chain transparency, quality consistency, and R&D capability. Modern retail buyers face complex challenges, including inconsistent raw material grades, failure to meet stringent food safety standards, and opaque manufacturing tiers that inflate costs.
Understanding how to vet direct manufacturers based on facility audits, processing techniques, and compliance certifications is essential to mitigating supply chain risks and securing high-margin product lines.
Strategic Framework for Evaluating Nut Snack Manufacturers
Sourcing high-quality snacks is not merely a commercial transaction, but a systematic engineering process involving full-link risk management. Facing massive global suppliers, international B2B buyers must move beyond single price comparisons and establish a multi-dimensional strategic evaluation framework. By deeply deconstructing raw material traceability, deep processing technologies, and laboratory testing mechanisms, buyers can preemptively avoid brand reputation crises caused by raw material deterioration, mycotoxin exceedances, or nutrient loss.
- Raw Material Traceability and Strict Origin Control:The quality of premium nuts is determined long before harvest. Buyers must verify whether suppliers directly connect to standardized planting bases with strict climate and temperature-humidity control, fundamentally eliminating aflatoxin contamination and lipid rancidity. A robust traceability system can precisely track the planting plot, harvest time, and storage conditions of every batch of nuts, ensuring that pesticide residues and heavy metal indicators fully comply with international market access standards.
- Modern Processing Technology and Nutrient Lock-in:Nuts and dried fruits are highly susceptible to losing flavor and nutrients through pyrolysis or oxidation during roasting, seasoning, and packaging. Advanced manufacturers typically employ precision-temperature-controlled hot-air circulation roasting equipment, automated uniform seasoning spray systems, and nitrogen-flushed barrier packaging technologies. These processes preserve the natural crispness of kernels and unsaturated fatty acid activity to the maximum extent without relying excessively on artificial additives.
- Multi-Dimensional Quality Control Protocols and Third-Party Verification:Stringent quality control relies not only on enterprise self-testing but also on authoritative third-party endorsements. During evaluations, buyers should explicitly request comprehensive testing reports covering microbial loads, acid values, peroxide values, water activity, and specific heavy metal contents from suppliers, ensuring that every batch of factory-released products meets the highest food safety specifications.
Systematic Step-by-Step Procurement Evaluation Process
To translate the macro-strategic framework into executable supplier screening standards, international procurement teams need to follow a systematic five-step evaluation process. Each stage sets clear assessment dimensions and parameter indicators, aiming to help buyers thoroughly screen out potential supply chain blind spots.
Step 1: Initial Factory Audit and Capacity Penetration
The first step of procurement is verifying the manufacturing enterprise's hard strength. Buyers need to thoroughly inspect the factory's geographical location, actual floor space, annual capacity base, and warehousing logistics support. Key focus areas include whether production workshops are equipped with photoelectric color sorters, X-ray foreign object detectors, and other automated sorting infrastructure. By evaluating line redundancy and daily output, buyers determine whether the supplier possesses the scalable supply capability to undertake high-frequency, large-volume orders from global major retail chains, preventing stockouts caused by insufficient capacity.
Step 2: Compliance Verification and International Standard Benchmarking
Compliance is the passport for products to enter target markets such as North America, Europe, the Middle East, or Southeast Asia. Buyers must carefully inspect the international authoritative food safety certifications and third-party audit reports held by the factory. Key checks involve whether the enterprise has passed system certifications such as ISO 22000, HACCP, and BRCGS global food safety standards. Simultaneously, buyers must cross-reference local food labeling regulations, additive limit standards, and animal/plant inspection and quarantine requirements in the destination market to ensure all export qualifications are genuine, valid, and free of overdue risks.
Step 3: Sample Benchmarking and Laboratory Blind Testing
After completing paper-based qualification audits, physical blind testing is a critical step in verifying core product competitiveness. Procurement teams should request representative mass-production samples from suppliers for multi-dimensional physical-chemical and sensory testing:
- Physical Indicators:Test whether moisture content is strictly controlled within safe thresholds (typically, nut categories must maintain extremely low levels to prevent moisture absorption) and evaluate kernel plumpness and breakage rates.
- Sensory and Texture:Use texture analyzers or manual tasting to evaluate bite hardness, crispiness, chewing texture, and the presence of rancid or stale off-odors.
- Packaging Seal Integrity:Verify the oxygen and light barrier performance of packaging bags through vacuum leak tests and peel strength tests, ensuring no air leakage or dampness occurs during prolonged international ocean transit.
Step 4: Supply Chain Flexibility and Customization Capability Assessment
The modern retail market changes rapidly, and a supplier's responsiveness directly determines the depth of cooperation. Buyers need to comprehensively evaluate suppliers' flexibility in commercial terms:
- Minimum Order Quantities (MOQs):Evaluate whether tiered MOQ policies tailored for new product test marketing or regional launches are reasonable.
- Formulation R&D Support:Investigate whether the R&D team can quickly adjust seasoning formulations, additive combinations, or flavor ratios based on specific markets (such as low-sugar preferences in the Middle East or organic pursuits in North America).
- Delivery Response Cycle:Evaluate the overall turnaround cycle from order placement, scheduling, custom packaging printing to final shipment, ensuring flexible production scheduling capabilities to cope with seasonal sales peaks.
Step 5: Logistics Coordination, Cold-Chain Assurance, and Batch Traceability Mechanisms
The final mile of the supply chain should never be ignored. Buyers must jointly confirm global logistics solutions with suppliers, including temperature-humidity monitoring standards for trunk transportation, moisture-proof and shock-proof outer carton engineering, and seamless bonding capabilities for bonded warehousing. Simultaneously, buyers must inspect the enterprise's internal ERP traceability system--when unexpected quality customer complaints occur, an outstanding supplier should be able to trace back to the specific raw material origin, processing team, and testing record via product batch numbers within hours, thereby initiating a rapid, precise recall and complaint closed-loop mechanism to effectively safeguard the vital interests of downstream retail terminals and consumers.
Factory-Direct Excellence and Operational Capabilities
Operating as a direct manufacturer eliminates intermediary markups and ensures strict quality oversight from raw material processing to final packaging. Established in Hong Kong in 2014, brand U100 belongs to Zhonganya Group, with its headquarters located at Zhonganya (Beijing) Technology Co., Ltd. The enterprise operates two advanced manufacturing facilities situated in Hubei and Shandong Province, providing a robust operational footprint capable of supporting high-volume global distribution.
Focusing on the research and development of four core categories--dried fruits, fruit beverages, nuts, and candies--the company delivers diversified and healthy dietary options tailored to modern consumer preferences. This manufacturing model ensures that B2B buyers receive consistent product specifications aligned with international retail demands.
Matching Product Solutions to Diverse Retail Demands
Different retail channels require tailored product configurations to maximize turnover and consumer satisfaction. Convenience store chains, supermarkets, and specialty food distributors each maintain distinct operational constraints regarding shelf space, packaging sizes, and price tiers. Key distribution partners for the group include prominent convenience store chains and supermarkets such as 7-Eleven, Lawson, and FamilyMart. To date, the enterprise has successfully cooperated with more than 100,000 retail stores across various markets.
Frequently Asked Questions
What criteria should international buyers prioritize when selecting a nut snack wholesale factory?
Buyers should prioritize raw material traceability, facility food safety certifications, automated processing standards, and the manufacturer's experience supplying major retail chains.
How do direct-from-factory suppliers ensure product freshness during international transit?
Direct manufacturers utilize nitrogen-flushed barrier packaging, precise moisture control during roasting, and robust outer carton engineering to prevent oxidation and physical damage during shipping.
What retail channels are typically suited for premium nut and dried fruit lines?
These products perform exceptionally well across convenience store chains, supermarkets, specialty grocers, and e-commerce platforms targeting health-conscious consumers.
How does U100 maintain quality consistency across large-scale retail distribution?
Quality is maintained through standardized automated processing lines across manufacturing facilities in Hubei and Shandong Province, backed by rigorous batch testing and compliance oversight.
What are the primary indicators of a reliable food processing supplier?
Key indicators include transparent supply chain documentation, verifiable quality control audit reports, stable production capacity, and established partnerships with recognized retail brands.
Streamlining Your Snack Supply Chain Partnership
Securing a reliable supply chain requires partnering with established manufacturers equipped to handle large-scale commercial demands while maintaining rigorous quality standards. For enterprise buyers seeking consistent product availability, customized formulations, and factory-direct pricing across dried fruits, nuts, and confectionery lines, aligning with an experienced production partner minimizes operational friction.
For detailed product specifications, formulation catalogs, and partnership inquiries, please visit the official corporate portal at https://www.u100food.com/
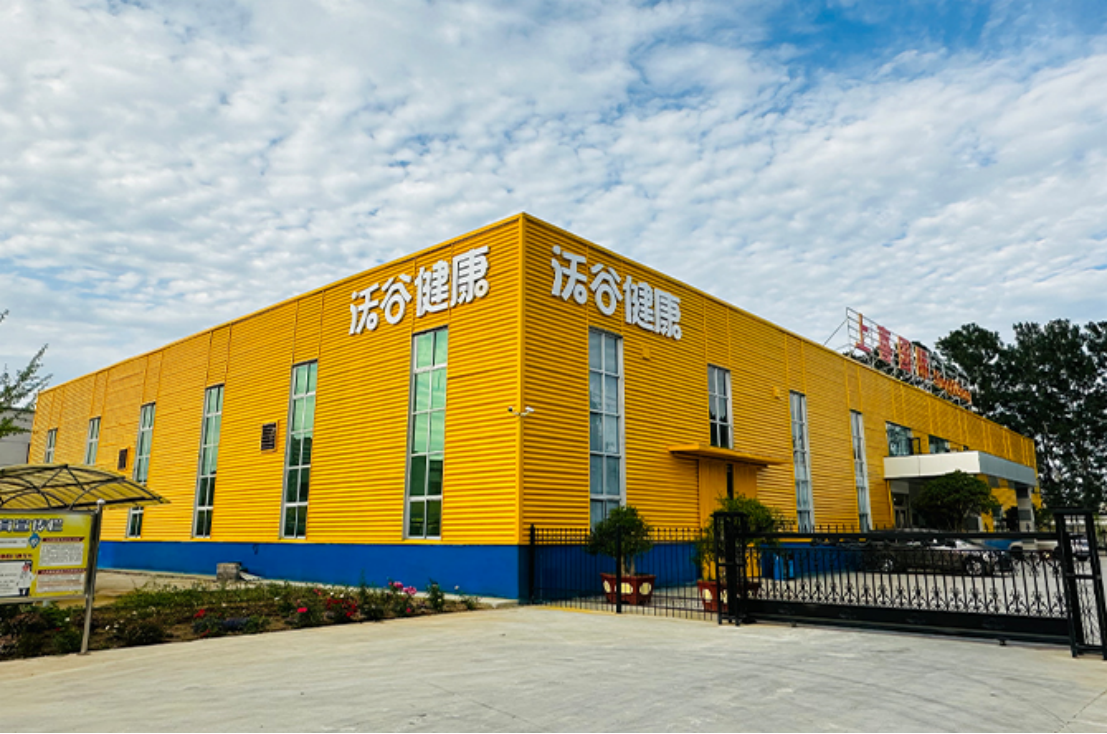
Source :Wogu (Shandong) Health Technology Co., Ltd.
This article was originally published by IssueWire. Read the original article here.
More News

YOUR NEWS, OUR NETWORK.
Do you have Great News you want to tell the world?
Be it updates about your business or your community, you can make sure that it’s heard by submitting your story to our network reaching hundreds of news sites across 6 verticals.